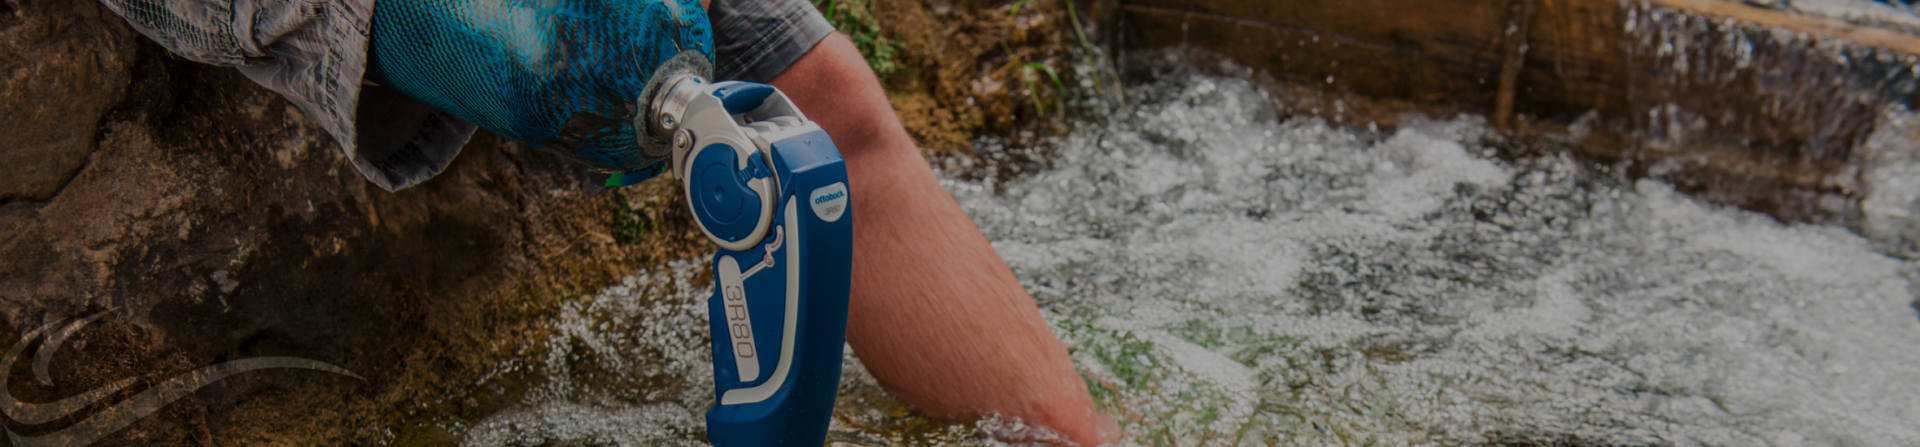
When it comes to freedom of movement, Ottobock is there to help. As a renowned and internationally active manufacturer of high-quality prostheses, orthoses, wheelchairs and exoskeletons, the manufacturer from Duderstadt helps many people to manage their everyday lives safely and comfortably. As no two bodies are the same, the company relies on flexible production processes. To achieve this, it relies on top MES as a modern manufacturing execution system.
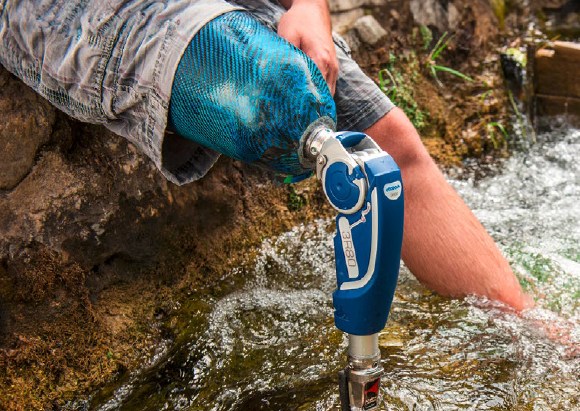
Ottobock helps people to maintain or regain their freedom of movement. The internationally active company from Duderstadt produces orthoses, prostheses, wheelchairs and exoskeletons. The secret of its success: the excellent quality of its products. Heinrich Popow also knows about this. In 2016, the top athlete jumped a sensational distance of 6.77 meters with a leg prosthesis from the family-run company in Lower Saxony – a world record for people with disabilities at the time! Founded in 1919, the German manufacturer now sells its high-quality solutions worldwide – and achieved a turnover of around 1.3 billion euros in 2022 with around 9,000 employees in more than 60 countries. To ensure that this remains the case, the company continues to focus on innovation, high quality standards and modern production.
However, production at Ottobock is very complex: a broad product portfolio meets the need to be able to adapt the solutions specifically to the future users.
“After all, no two bodies are the same. That’s why off-the-shelf solutions don’t fit all people,” explains Patrick Ehlers, Application Manager Production Planning at Ottobock.
In addition, production is usually organized in several stages and consists of a wide variety of manufacturing processes. For example, so-called custom-fit parts are created in a multi-layered workshop production process: These are individual components that orthopaedic technicians assemble into more complex solutions, such as prostheses. Ottobock also has its own final assembly facility for more standardized products. The batch sizes vary considerably in some cases, ranging from five to 1,000 workpieces per production order. Until recently, Ottobock used various modules and features of SAP ECC 6.0 EHP 8 to organize this production, but there was no integrated Manufacturing Execution System (MES) that would enable paperless operation and consolidate all important operating and machine data.
“There were major deficits here, particularly in component production – also because this was previously more of a manual process. At the same time, however, increasing competition meant that there was ever greater pressure to produce more cost-efficiently,” reports Thomas Einecke, Business Process Specialist at Ottobock. “That’s why we wanted a modern solution for fitting part production that records and provides all important information in digital form. It also needed to integrate as seamlessly as possible into our existing SAP landscape.”
While searching for a suitable solution, Ottobock came across the SAP add-on top MES from IT specialist top flow. The Duderstadt-based medical technology manufacturer was very quickly won over by its wide range of functionalities and application options. In addition to its complete integration into SAP, this also included the ability to record operating and machine data and use this as the basis for Overall Equipment Effectiveness (OEE) – as well as the option to establish a digital worker dialog.
“And finally, the fact that Ottobock was already successfully using their reporting and analysis tool top SE16XXL spoke in favor of top flow – and was therefore a trusted partner,” says Mr. Einecke, summing up the decision.
Once the partner had been determined, the companies formed a joint project team – consisting of consultants from top flow, supplemented by management and IT employees as well as key users from Ottobock. Together, the team outlined how the store floor in component production should be organized in the future. They initially focused on the main plant in Duderstadt.
They also determined where individual software adaptations would be necessary.
“It turned out that, among other things, we still had to design new interfaces to connect our AHP quality assurance system to the MES,” reports Mr. Ehlers.
Thanks to the close collaboration between Ottobock and top flow, the project team was able to fully digitize component production within a year.
Today, workers no longer need slips of paper. Instead, the company stores the worklists derived from production planning directly in the MES. At the workstations equipped with terminals, the workers can then freely choose from this worklist. The system supports them by displaying all the production documents required for the next production step, such as relevant technical drawings, product specifications or a deadline. Control between individual downstream production stages is also largely automated via the system. This is done via “feasible” worklists. The worker of a downstream production step only begins further processing as soon as the system releases it. To avoid idle times, the workers can freely help themselves to the “feasible” worklists that are always available in abundance
. Production is thus controlled via a pull system in which the workers retain control over the fine control.
The MES also makes work easier for the workers. If machines break down, they can report this digitally to the foreman. In contrast to the initial situation, they no longer have to actively search for the foreman in the event of a malfunction – an often time-consuming and therefore inefficient undertaking. In addition, workers can use the MES to conveniently trigger Kanban processes from their workstation and order additional consumables – for example, if there is an increased demand due to increased scrap.
For the targeted management and continuous improvement of production control, the project team implemented various dashboards with which they can monitor important key figures on machine utilization, downtimes and occupancy times, excess consumption, faults, etc.
“Overall, this makes production much more transparent. Controlling can also use the key figures to determine higher-level parameters such as OEE,” says Mr. Einecke, explaining the associated benefits.
Since going live in March 2022, Ottobock has had a state-of-the-art, networked production system for manufacturing its components. Thanks to more efficient production planning, the company has been able to optimize capacity utilization, reduce costs, and simultaneously improve quality in a sustainable manner. The new performance metric systems also help the company identify common sources of error more quickly in the future and thus gradually eliminate them.
Mr. Ehlers explains: “With this new solution, we’re securing our long-term competitiveness. Not only does it provide useful information for management, but it also supports our workers in their day-to-day tasks.” Since the system is already proving successful at the main plant in Duderstadt, Ottobock is already planning its rollout to other locations. Thomas Einecke: “Next, we want to introduce the system in Bulgaria. In the long term, however, every plant should benefit from the digitized shop floor.”
Location: Duderstadt (Headquarters)
Portfolio: Prosthetics, orthotics, exoskeletons, and wheelchairs
Revenue: approx. 1.3 billion euros (2022)
Founded: 1919
Employees: over 9,000 (2022) in nearly 60 countries
Website: www.ottobock.com
top flow GmbH


